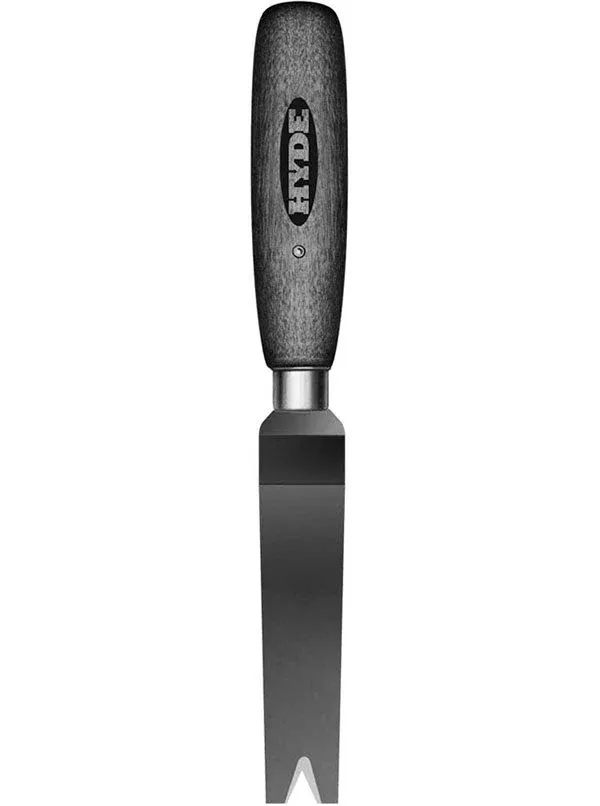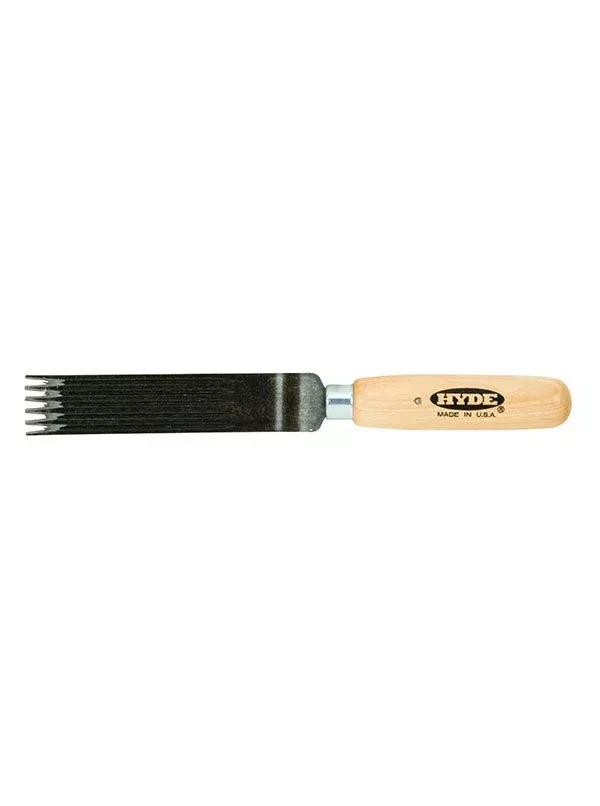
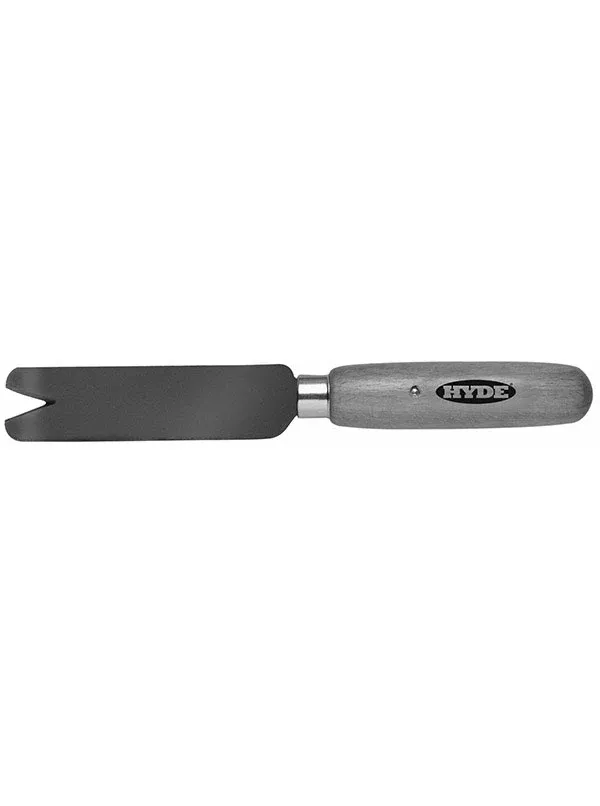
Is this the right tool for your job?
✕CHOOSE A DIFFERENT TOOL WHEN
- Contoured and crowned surfaces — a wide, square-tipped straight lifts its notch off the surface where it curves; that is the curved-tip 66030’s job, or an offset’s.
- Long convex pulls where hand clearance governs — the offset 66090 keeps the knuckles clear through a stroke the straight handle cannot.
- Tight, close-quarters detail — the narrower straight (66330) works closer than a full inch of width allows, and the compact 66030 is smaller still.
- Throughput vent-trimming of production tread rows — the five-groove pin trimmer (65060) clears the swath; the straights take the detail.
- And it is not a repair knife — it finishes healthy parts; injured-casing work is the K770 skiver (61350) and the H2T taper point (61260), other lines.
Jobs this tool does
EXACT JOB METHODS FOR HYDE №66060✓ Job guideChoose Straight vs Offset for Curved WorkOPEN JOB GUIDE →✓ Job guideHow to Deflash Molded Rubber GoodsOPEN JOB GUIDE →✓ Job guideFinish a Retreaded Tire After CureOPEN JOB GUIDE →✓ Job guideGang-Trim Tread Vents on a Production LineOPEN JOB GUIDE →
VIEW 3 MORE DOCUMENTED JOBS
✓ Job guideTrim Heavy Flash from Large Molded PartsOPEN JOB GUIDE → ✓ Job guideTrim Mold-Joint Flash from a TireOPEN JOB GUIDE → ✓ Job guideTrim Vent Spews on a Cured TireOPEN JOB GUIDE →
For these jobs—use this instead
THE JOB, THE REASON, AND THE BETTER TOOL✕ Contoured and crowned surfacesA wide, square-tipped straight lifts its notch off the surface where it curves; that is the curved-tip 66030’s job, or an offset’s. BETTER TOOL Straight V-Trim Curved Tip Knife H212 66030 →✕ Long convex pulls where hand clearance governsThe offset 66090 keeps the knuckles clear through a stroke the straight handle cannot. BETTER TOOL Offset V-Trim Knife H222, 3-1/2″ x 3/4″ 66090 →✕ Tight, close-quarters detailThe narrower straight (66330) works closer than a full inch of width allows, and the compact 66030 is smaller still. BETTER TOOL Straight V-Trim Knife 3787A, 3-15/16″ x 66330 →✕ Throughput vent-trimming of production tread rowsThe five-groove pin trimmer (65060) clears the swath; the straights take the detail. BETTER TOOL Offset Pin Vent Trimmer Knife H1357, 5″ 65060 →
VIEW 1 MORE JOB REDIRECT
✕ Injured-casing repairAnd it is not a repair knife — it finishes healthy parts; injured-casing work is the K770 skiver (61350) and the H2T taper point (61260), other lines.BETTER TOOLFlexible Skiver Knife K770, 4″ x 13/16″ 61350→
How the pros run it
01
Use the flank as a reference plane
The inch of width is there to keep the blade planted — hold it flat and let the broad bearing surface do the steadying; rocking the blade wastes the width. Never lift the trailing edge. As with every V-trim, raising the back to force the cut drives the notch walls into the surface and gouges it; the geometry protects the surface only when the flanks ride flat. Pull the notch along the protrusion, not into it — a running shear that feeds each spew and the flash ridge into the V. Two hands on heavy flash — the .065″ blade holds its plane under real pressure, which is why the line runs this stiffness and not a flexing one. Match the tool to flat, broad work — on tight contours the wide flat blade and its square tip lift off the surface at the tangent, and the job crosses to the curved-tip straight (66030) or an offset. Sharpen the notch on its walls with a slip stone or fine tapered file following the V, burr stropped off the outside face; a flat bench stone used alone rounds the flanks and un-designs the knife (authored trade knowledge; no Hyde maintenance text). High-carbon steel: dry it after wet work.